
You should know that about 70% of processing delays stem from manufacturability issues during the design phase. To prevent this issue, you must pay close attention to the design of the parts. An excellent CNC part requires not only outstanding modeling but also design that adheres to the physical limitations of cutting tools and relevant standards (such as ISO 2768 and ASME Y14.5). This ensures that your parts can be manufactured successfully. This guide will break down specific design rules in detail, allowing you to understand and operate intuitively.
What Makes CNC Part Design Different?

Unlike 3D printing, sheet metal fabrication or injection molding, CNC machining is a subtractive manufacturing process. CNC parts are gradually cut from a solid block of metal or plastic blank using tools such as milling cutters, drill bits, and turning tools. Therefore, when designing CNC parts, you cannot just consider whether the CAD model looks good; you also need to take into account multiple factors:
Tool Access

Cutting tools are cylindrical, so they must extend from a certain direction to cut. The tool cannot reach geometric features that are obstructed, enclosed, or hidden deep within the workpiece. Therefore, CNC machines cannot produce parts with closed internal cavities.
Tool Geometry

The tool is round, so the internal corners of the workpiece will always have rounded corners, and it is impossible to create perfectly sharp internal right angles. The length-to-diameter ratio of the tool also affects the depth of the workpiece cavity. Moreover, if the tool extension is too long, chatter will occur, which will also reduce machining accuracy and surface quality.
Workpiece Rigidity

As you know, parts must be securely clamped before machining. Workpiece structures that are too thin or too suspended will vibrate, deform, or even fly out under cutting forces. Therefore, when designing, you also need to consider how to securely clamp the workpiece.
Only by understanding these three underlying principles can your designs move from “modeling” to “manufacturability.” All subsequent design rules are merely extensions of these principles.
Core CNC Design Rules at a Glance
I’ve prepared this quick reference guide to CNC machining design guidelines for you, which will give you a clear understanding of the design rules for CNC parts. You can refer to it directly in the future.
| Feature | Recommended Guideline | Why It Matters |
| Internal corner radius | ≥ 1/3 cavity depth | Allows the use of larger cutting tools; better surface quality |
| Pocket depth | ≤ 4x pocket width | Reduces tool deflection and chatter |
| Wall thickness | Metals: about 0.8 mm+ Plastics: about 1.5 mm+ | Prevent vibration, warping, breakage |
| Hole diameter | Prioritize standard drill bit sizes | Reduces tooling cost |
| Thread length | 1.5x to 3x nominal diameter | Excessively deep threads usually only increase costs; they do not necessarily increase strength |
| Tolerances | Only tighten functional features | Tight tolerances increase inspection and machining cost |
Core Design Guidelines
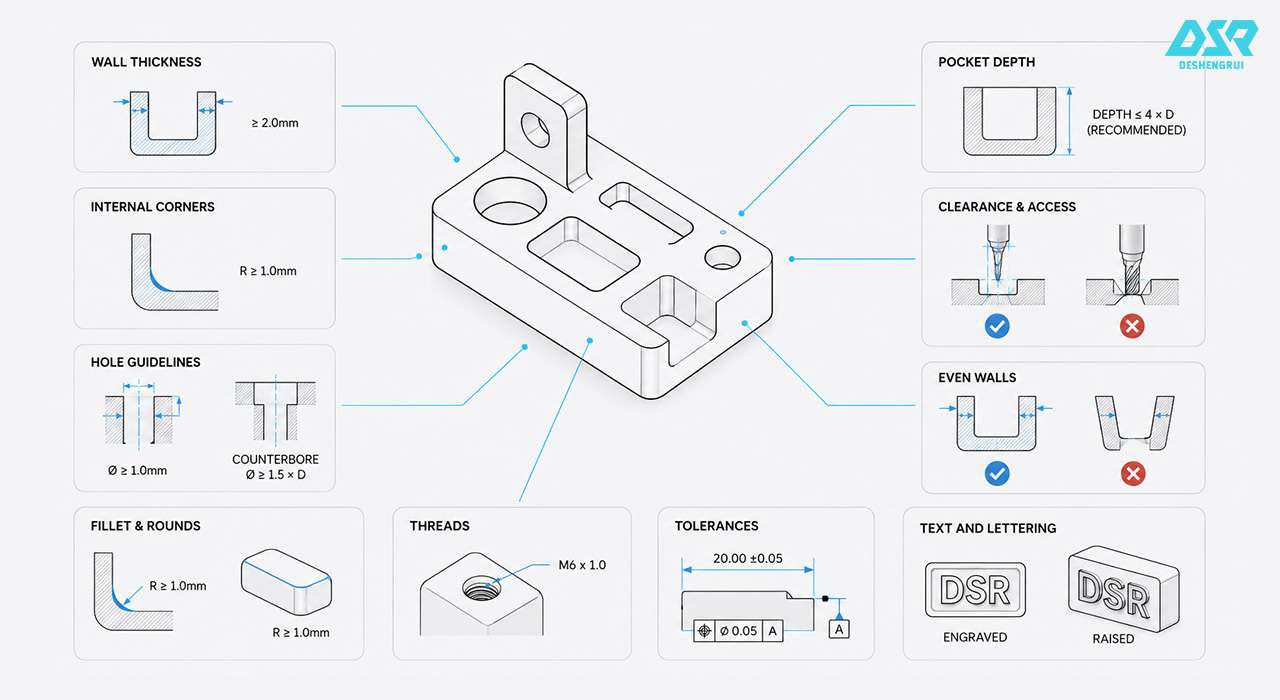
Next up is the highlight of this entire guide. I will analyze the design rules of CNC parts in detail to help you better understand these core points.
Internal Edges & Radii

In CNC machining, the internal corner radius is a design detail that is often overlooked. However, it often directly affects cost and machining difficulty.
Recommendation: 1/3 of cavity depth (or greater)
In CAD design, you can draw perfect 90° sharp internal corners. However, in actual machining, since milling cutters are typically cylindrical, the rotating cutting tool naturally leaves rounded corners during the cutting process. Therefore, unless using electrical discharge machining (EDM) or other special processes, it is difficult to directly machine truly sharp internal corners.
A better approach is to add appropriate radius to internal corners during the design phase. The larger the internal corner radius, the larger and more rigid cutting tools you can select for machining. At the same time, the entire cutting process will be more stable, and the surface quality of the part will be excellent.
Here’s a practical design principle: try not to make the inner corner radius too small, preferably slightly larger than the tool radius, and appropriately increase it as the cavity depth increases.
Formula:
$$R_{\text{internal corner}} \ge 1.3 \times R_{\text{tool}}$$
Vertical corner radius
Vertical corner radius refers to the internal corner radius between the sidewalls of pockets, slots, and cavities. When designing these internal corners, it is recommended not to make the radius too small, preferably larger than the tool radius. If sharp 90-degree internal corners are needed, you can consider using dogbone relief or T-bone relief.
Floor radius
Floor radius refers to the transition fillet between the side wall and the bottom surface. If the floor radius is designed to be too small, the tool needs to perform more precise machining on the bottom edge. This can easily increase the overall machining time. However, the floor radius should not be increased arbitrarily. If the bottom surface needs to fit perfectly against other parts, it is necessary to specify which areas allow for fillets and which areas must maintain flat contact.
Wall Thickness

Wall thickness is a critical parameter in CNC part design. However, during actual machining of thin-walled parts, if the wall thickness is too thin, issues such as vibration, deformation, and even outright fracture can easily occur. This is because the cutting tool generates forces during machining, and thin-walled structures have relatively weak ability to withstand forces, making them prone to the aforementioned problems.
Generally, the minimum wall thickness for metal parts can be 0.8 mm or more, and plastic parts are recommended to be at least 1.5 mm or more. Of course, these are merely general guidelines and not absolute standards.
When designing, you also need to consider materials, wall heights, part shapes, processing directions, and tolerance requirements. For example, aluminum alloy is more stable than plastic. Plastics such as PEEK, nylon, and ABS are more prone to thermal deformation during machining, so these materials typically require more conservative wall thickness designs.
I’ll give you a simple judgment scheme: the higher the wall, the thicker it should be.
If you want to make the parts easier to machine while ensuring quality, you must choose an appropriate wall thickness. For functional parts, a more conservative wall thickness design is usually more reliable.
Cavities & Pocket Dept

Cavities and pockets are common structures in CNC parts, such as grooves, cavities, mounting slots, and weight reduction slots. When designing these features, the most important factor to consider is depth.
A common design rule of thumb is that the pocket depth should not exceed four times the pocket width.
Formula:
$$\text{Depth ratio}=\frac{\text{cavity depth}}{\text{tool diameter}}\le 4$$
If the cavity is deep and narrow, the tool must extend very long to reach the bottom. The longer the tool extends, the lower its rigidity. This easily causes the tool to shake or chatter during machining.
Another challenge in deep cavity machining is chip removal. If the chips generated during cutting are not removed in time, they will accumulate inside the cavity. This not only interferes with the normal cutting of the tool, but may also scratch the machined surface.
Therefore, my suggestion is that if the part function allows, it is recommended to reduce the pocket depth as much as possible, or change the deep cavity to a more open structure. For example, widening the opening, adding fillets, and so on.
Holes

Holes are also one of the most common features in CNC parts, but the design of holes directly affects the machining cost, accuracy, and lead time of parts.
When designing holes, you should prioritize using standard drill bit sizes. This is because standard hole diameters are easier to machine and inspect. If non-standard hole diameters appear in the design drawings, the factory will need to use milling cutters for interpolation, custom tools, or secondary machining to complete the work, which will naturally increase costs. Therefore, for conventional parts, unless a special size hole is truly required for functionality, you should try to use metric or inch standard hole diameters.
In addition, you also need to control the depth of the hole. It is generally recommended that the depth of ordinary holes should not exceed 4 times the hole diameter. If it exceeds 8-10 times the hole diameter, it becomes deep hole machining, and the processing difficulty significantly increases. Moreover, during deep hole machining, chip evacuation, cooling, and tool deflection all become issues, especially for materials such as stainless steel and titanium alloys.
Another thing you should note is that through holes are usually easier to machine than blind holes. Through holes facilitate chip removal and make it easier to ensure the integrity of the hole. Blind holes, on the other hand, require consideration of the bottom shape, because blind holes machined with regular drill bits typically don’t have completely flat bottoms, but rather retain the drill point angle. If the design requires flat-bottom holes, additional use of end mills or special tools will be needed during machining, which increases machining time.
As for holes that require high-precision fit, such as pin holes and bearing holes, I do not recommend just using ordinary drilling to complete them. You can specify precision machining requirements on the drawings and mark tight tolerances for critical holes.
Of course, if you want to learn more about drill bits, you can also check out this article: Best Drill Bits for Metal.
Threads

Threads are a common assembly feature in CNC parts, mainly used for fixing, connecting, and positioning screws. When you design threads, it’s not about making the threads as deep as possible, but rather ensuring that the thread dimensions are standard, the depth is reasonable, and the machining path is clear.
When designing, you should first use standard thread specifications, such as common metric threads or UNC/UNF threads. Additionally, the thread depth should also be controlled. Generally, an effective thread length of 1.5D to 3D can meet most assembly requirements (D refers to the thread diameter).
As for blind threaded holes, you need to pay attention to the bottom space. And the hole depth is slightly larger than the effective thread depth. This will also make the entire threading process more stable.
If the material of the parts is aluminum, plastic, or other softer materials, you should also consider thread durability. For threaded holes that are frequently assembled and disassembled, you can consider using threaded inserts, Helicoil, or wire thread inserts.
Tolerances

CNC machining tolerance can be said to be the most important factor in CNC design, and it also directly affects processing costs. Many designers are accustomed to setting extremely tight tolerances for all parts, but in actual manufacturing, not all areas of the parts require such high precision. It’s important to know that the tighter the tolerance, the higher the cost.
My suggestion is that you should only use tight tolerances for features that affect the assembly, movement, sealing, or positioning of parts. For example, you can specify strict tolerances for features such as dowel holes, bearing holes, mating surfaces, seal grooves, and locating steps. However, for features such as the outer edges of parts, non-contact surfaces, and general contour dimensions, using general tolerances (±0.125 mm) is sufficient.
Additionally, on the drawings, it is recommended to annotate critical dimensions separately, while using the default tolerance standard, such as ISO 2768, for ordinary dimensions. Of course, if the part involves multiple assembly relationships, you should also consider using GD&T, such as geometric tolerances for flatness and parallelism.
Just remember, the clearer the marked information, the more accurate the quotation, and the lower the communication costs.
Text and Lettering

There’s one more point that is often overlooked in design, which is text and lettering. In fact, text and lettering are commonly used in CNC parts for part numbers, brand logos, directional indicators, or serial numbers. When designing text, don’t just focus on the visual appeal.You also need to consider that these texts can be processed stably.
In CNC machining, engraved text is generally easier to machine than raised text. Engraved text involves carving text into the surface, where the cutting tool only needs to remove a small amount of material along the text path. Raised text refers to text that is raised, which means that a large area of material around the text must be milled away. This process takes longer and is more expensive. Unless you have special appearance or functionality requirements, engraved lettering is preferred.
Furthermore, the font should be kept as simple as possible. I recommend using clear sans-serif fonts, avoiding serif fonts, handwritten fonts, thin-line logos or complex patterns. For very small markings, you can consider processes like laser marking or silkscreen instead of insisting on using CNC machining.
Design for Fewer Setups and Easier Fixturing

This is also a point that many designers tend to overlook. In CNC machining, setup refers to the process of fixturing, positioning, and calibrating a part. Each additional setup of a part means that the operator needs to re-clamp the part, re-find the datum, and re-calibrate the tool path. This not only increases machining time but also increases the risk of dimensional errors.
For 3-axis CNC machining, when designing part features, you should try to ensure that the tool can enter vertically from above. Although 5-axis machining can handle more complex geometries, if the part can be manufactured on a 3-axis machine through simple design, it is typically less expensive and has more predictable lead times.
Therefore, when you design CNC parts, an important principle is: minimize the number of setups and make parts easier to be stably fixed. An ideal design would allow most of the part features to be machined from the same direction.
Consolidate Feature Orientation
You try to concentrate features such as holes, slots, and steps on the main machining surface of the workpiece, rather than scattering them on various sides. For example, if all features of a part are facing upwards, it can usually be machined in just one setup.
Minimize Back-Side Features
When designing parts, unless there are special requirements, you should try to avoid designing features such as holes or slots on the back of the part. If functionality allows, merging these features to the same side can directly save one process step.
Clamping Surface
In addition, fixturing also affects machining stability. Parts must have sufficient clamping surfaces, and not all external surfaces can be curved, thin-walled, or precision appearance surfaces. After all, if there are no suitable clamping positions, the factory may need to design custom fixtures, which would also increase costs.
Choose Materials with Machinability

In the entire machining process of parts, material selection is an important step. When you are selecting CNC materials, you cannot simply consider the strength or price of the material; you also need to understand the machinability of the material. A material with good machinability provides more stable cutting, less tool wear, and better control over surface quality.
Metal Materials

For example, aluminum alloy, especially 6061 aluminum, can be said to be the most common material in CNC machining. It is lightweight, has moderate strength, and good machinability, making it suitable for aluminum parts such as prototypes, aluminum shafts, and enclosures.
The same goes for brass, which has good machinability. Brass is suitable for making conductive parts, brass sleeves and precision small parts. There is also stainless steel material, which has better strength and corrosion resistance, and the stainless steel parts made of it also have excellent performance. However, the machining speed of stainless steel is generally slower than that of aluminum.
As for materials such as titanium alloy, tool steel, and hardened steel, although their material properties are very strong, they are also more difficult to process. They have higher requirements on cutting tools, cooling and processing parameters. When designing parts made of these materials, you should try to avoid features such as excessively deep pockets, small internal corners, and extremely thin walls, otherwise, the cost will be very high.
Quick Comparison Chart of Common Metals
| Material | Machinability | Relative Cost | Typical Applications |
| Aluminum 6061-T6 | Excellent | Low | Prototypes, structural parts, enclosures |
| Brass C360 | Excellent | Medium | Fittings, electrical components |
| Mild Steel 1018 | Good | Low | General structural parts |
| Stainless Steel 304 | Moderate | Medium | Corrosion-resistant parts |
| Stainless Steel 316 | Poor | Medium-High | Medical, marine environments |
| Titanium Ti-6Al-4V | Poor | High | Aerospace, medical implants |
Plastic Materials

ABS, POM, nylon, PEEK and other materials can all be CNC machined, but plastics are more susceptible to thermal deformation and are also more prone to deformation due to excessive clamping force. Therefore, when designing plastic parts, wall thickness should generally be more conservative than for metal parts, and thin walls, deep grooves, and high-precision holes require special attention.
| Material | Machinability | Relative Cost | Typical Applications |
| ABS | Excellent | Low | Housings, lightweight parts |
| POM (Acetal) | Excellent | Low | Gears, bushings, precision parts |
| Nylon (PA) | Good | Low | Wear components, insulators |
| Polycarbonate (PC) | Good | Medium | Transparent parts, covers |
| PEEK | Moderate | High | High-temp, medical, aerospace |
| PTFE (Teflon) | Moderate | Medium | Seals, low-friction parts |
* Of course, if you want to learn more specifically about the topic of material selection, you can refer to another article on this site: A Complete Guide to CNC Machining Material Selection. This guide can provide you with a more detailed analysis.
Surface Finish & Post-Processing

Surface-treated parts not only enhance their appearance but also affect the friction, sealing and other performance characteristics of the parts. For most CNC machined parts, as-machined finish can already meet functional requirements, and the part surface will retain slight tool marks. If the part also needs to serve as a sliding surface, sealing surface or high-precision mating surface, you can separately specify a finer surface roughness, such as Ra 3.2 μm or Ra 1.6 μm.
Edge breaks

Edge breaks on parts also require attention. After CNC machining, parts may have sharp edges or burrs. If not treated, these sharp edges or burrs may affect assembly or scratch operators. The common practice is that you can mark “break all sharp edges” on the drawing or specify chamfer, such as 0.2 mm, 0.5 mm.
Post-Processing

Post-processing methods for parts include anodizing, bead blasting, polishing, powder coating, etc. Different post-processing methods can bring different effects and properties to parts. And some post-processing can change dimensions or affect threads, holes and precision mating surfaces.
For you, it is best to understand the application requirements of the parts in advance and identify which surfaces require post-processing. For example, bearing holes, locating pin holes and sealing surfaces. If precision sitll need to be maintained after post-processing, then you need to specify the inspection status and masking requirements in the drawing. This can prevent assembly problems after the part has been post-processed.
CAD Files and Technical Drawings

Many people are still unclear that CAD files and technical drawings actually play different roles in CNC machining.
CAD files primarily define the 3D geometry of parts, such as external shapes, hole positions, grooves, curved surfaces, and assembly structures. Factories then generate tool paths based on the CAD model.
However, many specific manufacturing requirements cannot be expressed solely through 3D models in CAD files. For example, manufacturing needs such as critical tolerances, thread specifications, surface roughness, material grades, etc., are all annotated in technical drawings. Especially for parts with precision assembly requirements, technical drawings often provide more detailed part processing information than models.
My suggestion is that you use CAD files to express geometry and technical drawings to express manufacturing requirements. This allows the machining shop to understand the part’s function more quickly and provide a more accurate quote. This will allow the machining shop to understand the part’s function more quickly and provide a more accurate quote.
Additionally, I would like to say a few words about the format of the file. Common file formats include STEP, IGES, SLDPRT, and X_T. For CNC quotes and machining, STEP files are generally the most widely used. Technical drawings can use PDF. You must clearly indicate the material, quantity, units, scale, surface finish, and version number in the title block. Moreover, the information between CAD and drawings must be consistent.
DFM Checklist
Below, I will provide you with a detailed DFM Checklist for use in your daily design work.
Geometry & Wall Thickness
- Are all wall thicknesses above the recommended minimum values (metal ≥ 0.8 mm, plastic ≥ 1.5 mm)?
- Have fillets been added to all vertical internal corners?
- Does the inner corner radius comply with standard tool dimensions?
- Is the cavity depth of parts within the reasonable processing range of the tool?
- Have unnecessary deep narrow cavities been avoided?
Holes & Threads
- Do hole diameters match standard drill sizes?
- Are hole depths within 4× the hole diameter where possible?
- Are threads kept to standard sizes and reasonable depths?
- Have you avoided threading all the way to the bottom of blind holes?
Setups & Workholding
- Have the part features been integrated into the minimum number of machining directions as much as possible?
- Have unnecessary backside features been eliminated?
- Have critical mating dimensions been integrated into a single setup?
- Is there at least one flat reference surface for clamping?
- Has a conventional clamping area been reserved for vises or fixtures?
- Will thin-walled or cantilever structures deform under clamping force?
- Can symmetry be used to simplify positioning and reduce clamping errors?
Material Selection
- Does the selected material actually meet the actual working conditions of the part?
- Is there a material with better machinability that can meet the same technical requirements?
- Unless it is necessary to use higher specification materials, has 6061-T6 aluminum alloy been selected by default?
- If using a hard-to-machine material (titanium, 316), is the geometry simplified?
- Could a surface treatment replace a more expensive base material?
Tolerances & Surface Finish
- Are all dimensions defaulted to general tolerances (ISO 2768)?
- Are tight tolerances applied only to true mating dimensions?
- Have you avoided requiring a mirror finish on all surfaces?
- Could a surface treatment (anodizing, bead blasting) meet the requirement instead of a costlier material?
- Are critical sealing or sliding surfaces given a specific Ra value?
Common CNC Design Mistakes to Avoid
Here, I have also compiled a quick reference guide for common design errors for you. I believe it will be helpful for your part design.
| Common Error | Consequence | Correct Practice |
| Sharp internal corners | Cannot be milled; requires EDM | Add radii to internal corners |
| Deep and narrow cavities | Tool chatter, poor accuracy | Keep depth-to-diameter ratio ≤ 4:1 |
| Walls too thin | Deformation and vibration | Maintain minimum wall thickness |
| Threads tapped to the bottom of a blind hole | Tap breakage; part scrap | Leave thread relief space |
| Features scattered across multiple faces | More setups required | Consolidate feature orientations |
| Tight tolerances everywhere | Doubled cost | Tighten only at mating dimensions |
| No clamping surface | Requires custom fixturing | Leave a flat reference surface |
| Excessive polishing | Unnecessary secondary operation | Default to a standard finish |
Conclusion

Alright, that’s all about CNC part design. It’s important to understand that CNC part design is not just about completing the CAD model, but more importantly, you need to understand how this part will subsequently be machined, clamped, inspected, surface treated, and assembled.
Of course, design is only the first step—the part on the drawing still needs to be manufactured into a physical component. Our DSR company is an experienced CNC machining manufacturer that can rely on advanced CNC machining services to manufacture the parts you design. We will strictly control the tolerances of the parts and and offer a variety of surface finshes options. If you have needs, contact us quickly!
FAQ
Q1: Best software tools for designing parts for CNC machining?
A: Common CAD tools include SolidWorks, Fusion 360, Autodesk Inventor, Creo, CATIA, NX, and Onshape. And common CAM tools include Fusion 360 Manufacturing, Mastercam, PowerMill, SolidCAM, hyperMILL, and NX CAM.
Q2: Tips for designing aluminum parts for CNC machining?
A: 1. When designing CNC aluminum parts, you should pay attention to the rigidity, heat dissipation, tool accessibility and processing stability of the material.
2. Use appropriate wall thicknesses and sufficiently large fillet radii.
3. Holes, threads, and counterbores of aluminum parts should preferably use standard dimensions.
4. Pay attention to surface treatment allowance. Because anodizing, sandblasting or chemical plating may affect the dimensions and appearance of aluminum parts.
5. If parts require high strength or good machinability, common aluminum alloys such as 6061, 6082, or 7075 should be considered first.
Q3: How to design for CNC cutting?
A: A: When designing parts for CNC cutting, you need to consider three aspects: ‘tool accessibility, structural stability, and machining economics’.
At the same time, you must also take into account the clamping method, machining direction, tool length, material properties, and surface finish allowances. Additionally, you should minimize the number of times the workpiece needs to be flipped and reduce the number of complex features.


